8 PPM prismatic ESS module & PACK line

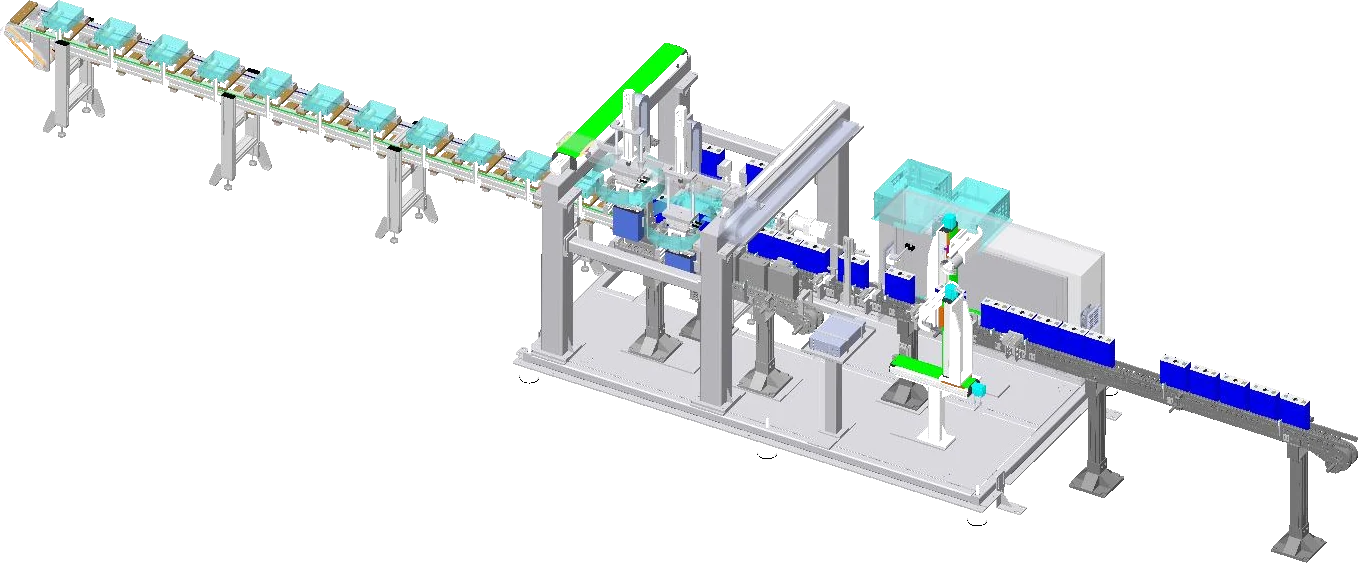
55 metres,
cell to storage.

8 PPM · 21 STATIONS · 3 SEGMENTS

Twenty-one stations in three segments take prismatic cells from the pallet to a tested, sealed PACK. Built around 314 Ah cells, with headroom for 587 Ah.

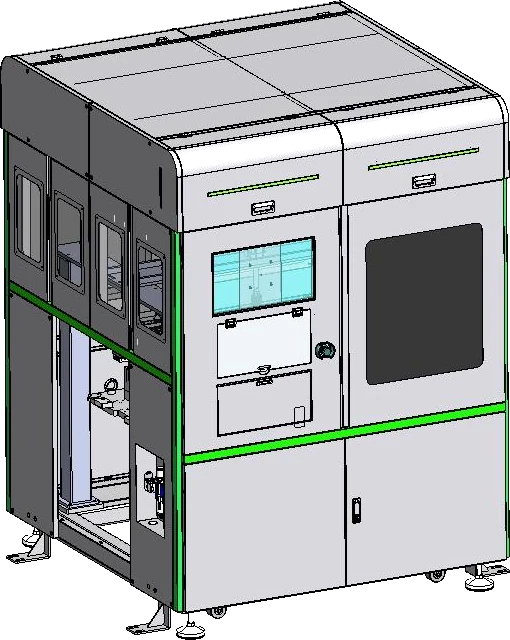
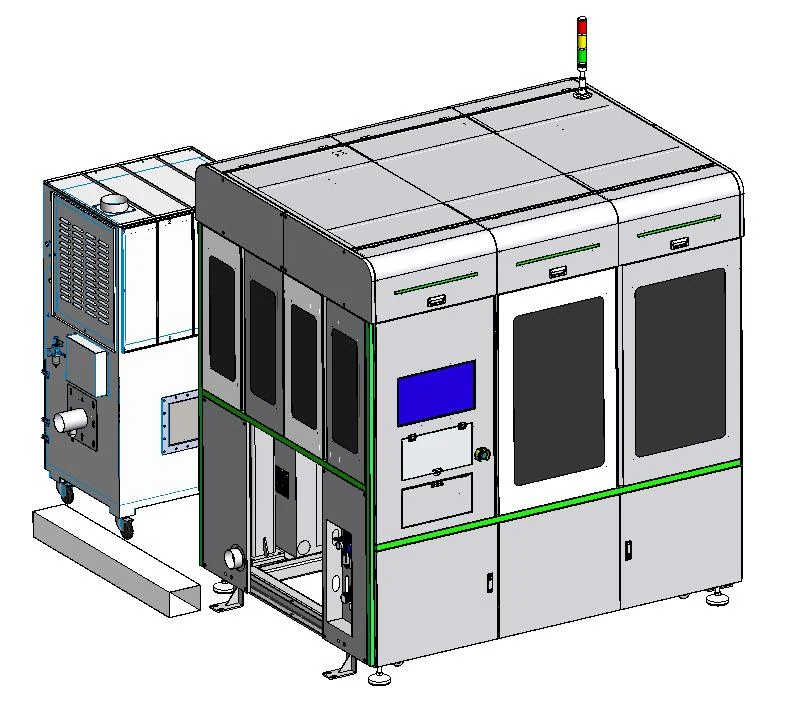
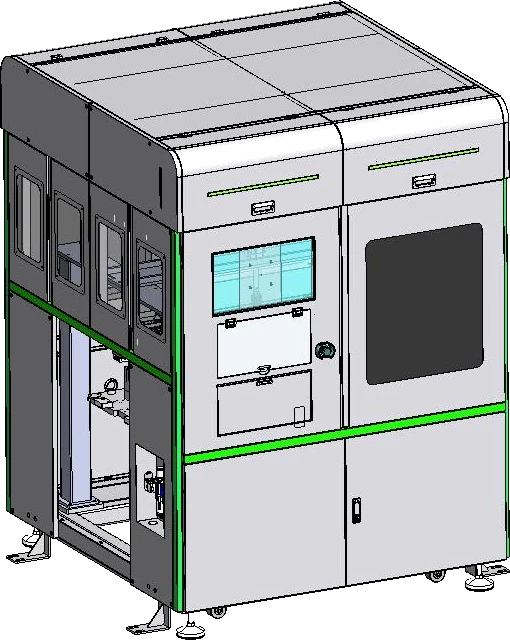
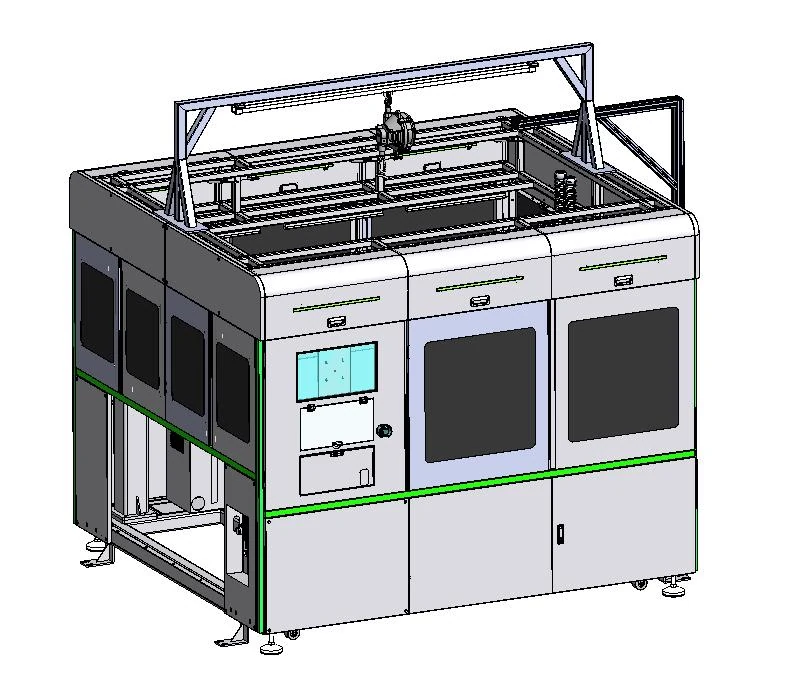
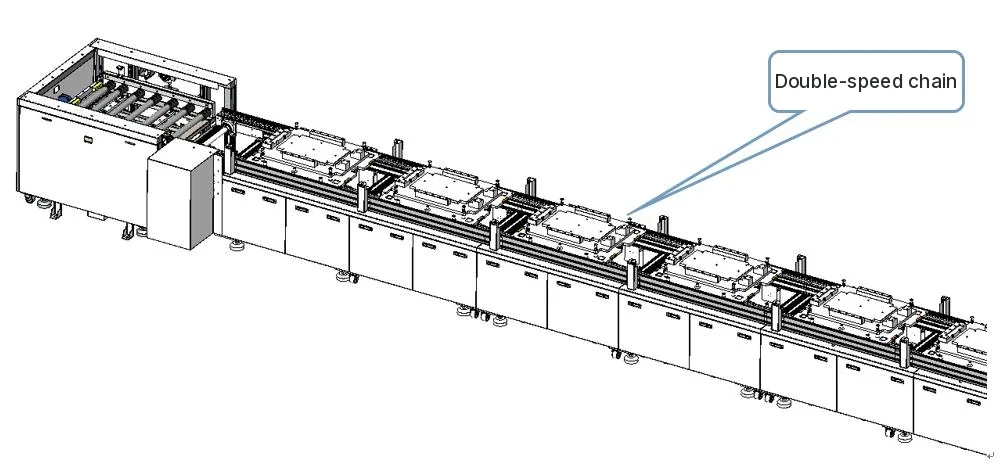
※ 3D views are illustrative white models

Takt
8PPM
One cell every 7.5 s
Footprint
55×9×3.5m
Excl. storage & aisles
Rated power
≤250kW
380 V, 3-phase 5-wire
Line yield
≥99%
Equipment-related
Cells
314→587Ah
Large-format ready
Stations / crew
21 / 21
Three segments

01 · Cell Processing

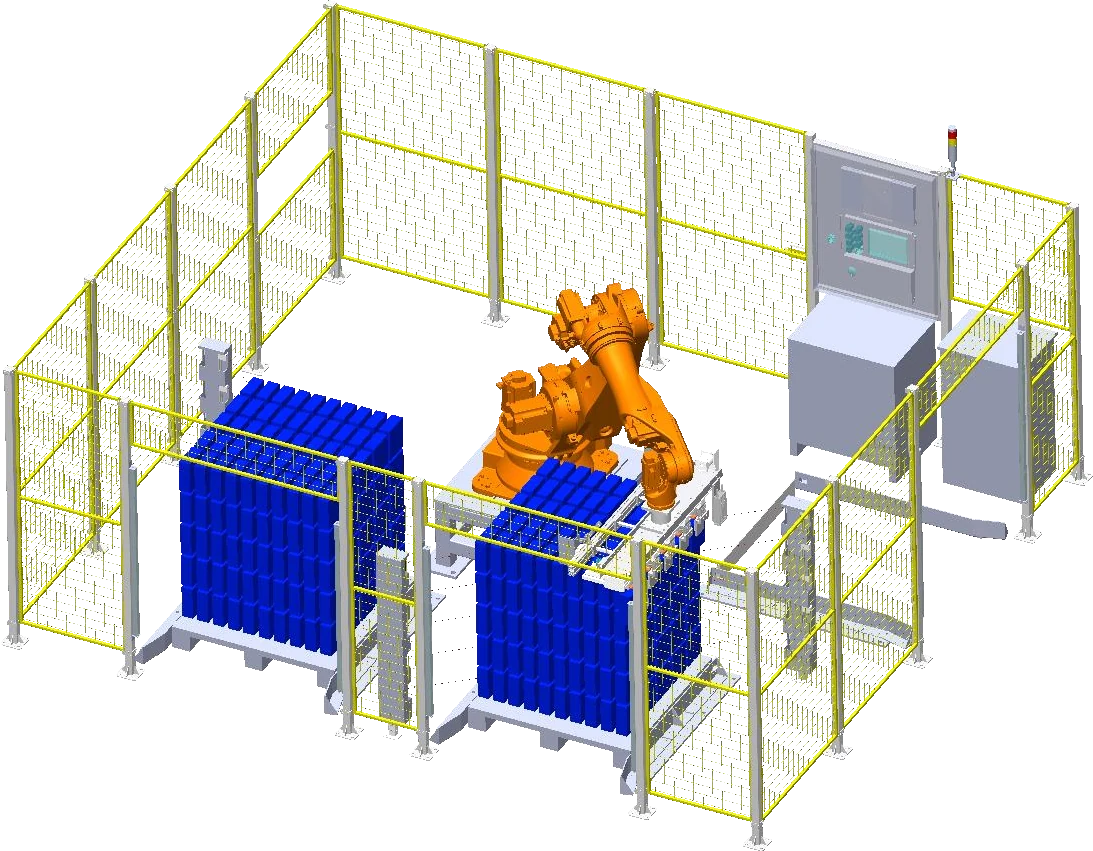
Robotic depalletizing. Every cell tested.

A 220 kg, ±0.06 mm six-axis robot with vision picks five cells at a time. Scanning, OCV testing and NG rejection run automatically, and gaps refill themselves.

  1. 01Full-pallet cell infeedManual
  2. 02Robotic depalletizingAuto
  3. 03Barcode scan / OCV testAuto
  4. 04NG reject / OK refillAuto
  5. 05Cell flipping & groupingAuto
  6. 06Cell adhesive applicationManual

3 operators in this segment

02 · Module Stacking & Welding

Twin stacking. Vision addressing. 6 kW laser.

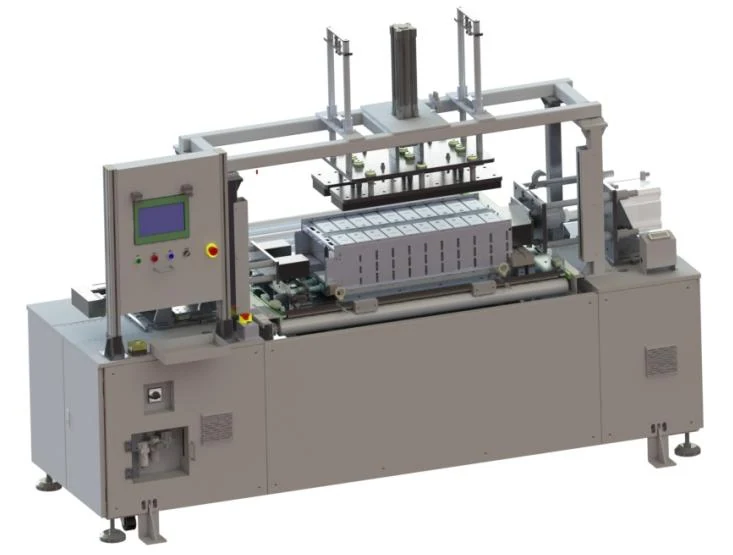
Twin servo presses (0–8000 N) either side of the line hold takt. One vision system locates terminals and checks polarity (±0.2 mm). A gantry galvo welder delivers ≥1.0 mm penetration and ≥1000 N pull strength, and every module passes EOL.

  1. 07Module stacking & pressing ×2Semi-auto
  2. 08Terminal addressingAuto
  3. 09NG rejectionAuto
  4. 10CCS / busbar placementManual
  5. 11Busbar laser weldingAuto
  6. 12Post-weld cleaning & inspectionManual
  7. 13Module EOL testAuto
  8. 14Module transferManual

6 operators in this segment

03 · PACK Assembly & Test

One straight line. Automated dispensing. Dual test.

After the cooling-plate leak test, a vision-corrected 3-axis dispenser lays thermal structural adhesive in the lower housing (±2 mm path, 5 % volume). Six two-sided assembly stations follow, then PACK EOL and full-pack leak testing.

  1. 15Cooling-plate infeedManual
  2. 16Cooling-plate leak testSemi-auto
  3. 17Lower-housing thermal adhesive dispensingAuto
  4. 18Module boxingManual
  5. 19PACK assembly stations ×6Manual
  6. 20PACK test stations ×2Semi-auto
  7. 21Finished PACK offloadManual

12 operators in this segment

Film · 0:30

The whole line
in 30 seconds.

From the first cell set in place to the full 55 m line: takt, key machines, compatibility and plant planning in one take.

Transcript
  1. Every 7.5 seconds,
  2. a cell is tested, sorted and stacked.
  3. 55 metres. 21 stations. One line, from cell to storage.
  4. Vision-guided robotic depalletizing.
  5. 6 kW laser welding.
  6. 2,800 V. Every module tested.
  7. Built for 314 Ah. Ready for 587.
  8. Size capacity and plant fit, before you order.
  9. Stratavolt.
  10. Request your line proposal.

Process

Two flows, 26 operations.
Automated where it pays off.

Quality-critical steps — test and sort, terminal addressing, laser welding, module EOL and adhesive dispensing — are automated. Assembly stays manual for flexibility across product variants.

  • Auto · 6
  • Semi-auto · 4
  • Manual · 16

Cell processing · Module stacking & welding

12 operations
  1. 01Depalletize & load cellsAuto
  2. 02Test & sort cellsAuto
  3. 03Apply cell adhesiveManual
  4. 04Glue & fit end platesManual
  5. 05Stack moduleManual
  6. 06Press & strapSemi-auto
  7. 07Address terminals / check polarityAuto
  8. 08Place busbars / CCSManual
  9. 09Laser-weld busbarsAuto
  10. 10Clean & inspect weldsManual
  11. 11Module EOL testAuto
  12. 12Module offloadManual

PACK assembly & test

14 operations
  1. 13Load cooling plateManual
  2. 14Cooling-plate leak testSemi-auto
  3. 15Dispense thermal adhesiveAuto
  4. 16Box modulesManual
  5. 17Fix modulesManual
  6. 18Install BMSManual
  7. 19Fit series copper barsManual
  8. 20Fit MSD & HV/LV connectorsManual
  9. 21Fit top coverManual
  10. 22Torque top coverManual
  11. 23Fit front panelManual
  12. 24PACK EOL testSemi-auto
  13. 25Full-pack leak testSemi-auto
  14. 26PACK offloadManual

About 21 operators in total

3Cell Processing
6Module Stacking & Welding
12PACK Assembly & Test

Cell processing: 1 loading, 2 adhesive. Module stacking & welding: 2 strapping, 1 busbar placement, 1 post-weld cleaning, 1 transfer, 1 reserve. PACK assembly: about 12, with two-sided stations.

See all 21 stations and the full layout →

Product & compatibility

Thirteen cells.
One module.

Built around a 1P13S reference module. Scroll to take it apart and see which station handles each part.

CELL

207×173×72mm

H × W × T, ±0.5 mm

MODULE RANGE

Height100–240Width150–370Length300–1000mm

PACK RANGE

Height100–250Width300–800Length600–1200mm

  • 08Terminal addressing · polarityAccuracy ≤ ±0.2 mm
  • 11Busbar laser welding6 kW · ≥1.0 mm penetration
  • 13Module EOL testDC 2800 V · ≥500 MΩ
  • 07End-plate gluing & fittingManual · twin stations
  • 03Cell scan / OCV±(0.01 % rdg + 3 dgt)
  • 07Servo press · steel strap0–8000 N · 300–1100 mm

Configurator

Before you sign,
size it for your plant.

Adjust takt, operating hours and OEE to estimate annual output. Enter your plant data to check footprint, floor load, power and air.

Simulation8 PPM · 7.5 sCells since you arrived 0
  • Auto
  • Semi-auto
  • Manual
CAPACITY ESTIMATOR

Capacity estimate

Cell format
Estimated annual output2.46GWh / yr2,448,000 cells · 188,308 1P13S modules= 8 × 60 × 20 × 300 × 85% × 1.005 kWhCell energy at 3.2 V LFP nominal. Estimate for planning only; not a performance guarantee
PLANT FIT CHECK

Plant fit check

    Request a proposal with these figures →

    Specifications

    Specifications & plant requirements

    Line
    EquipmentPrismatic ESS module & PACK assembly line
    Design takt8 PPM (counted in cells, 1P13S reference module)
    Reference cell314 Ah; designed with 587 Ah cells in mind
    Line yield≥ 99 % (equipment-related defects only)
    Stations21 numbered stations (incl. twin and multi-station groups)
    OperatorsAbout 21: cell processing 3, module 6, PACK about 12
    Plant requirements
    Power supply3-phase 5-wire 380 V ±5 %, 50 Hz, rated 250 kW
    Compressed air0.5–0.7 MPa, flow ≥ 3000 L/min
    Shielding gasNitrogen 0.5 MPa, 40 L/min
    Floor load≥ 800 kg/m²
    Footprint55 m × 9 m × 3.5 m (excl. warehouse & logistics aisles; adaptable to your plant)
    Product envelope (mm)
    HWL / T
    Cell 314 Ah207 ± 0.5173 ± 0.572 ± 0.5
    Module100–240150–370300–1000
    PACK100–250300–800600–1200

    Open the printable datasheet →

    FAQ

    What buyers and engineers ask first

    01

    How is the 8 PPM takt defined?

    Takt is counted in cells: 8 cells per minute, or one cell every 7.5 seconds. With the 1P13S reference module that is one module about every 97.5 seconds.

    02

    Which cell, module and PACK sizes are supported?

    The reference cell is 314 Ah (207 H × 173 W × 72 T mm, ±0.5 mm), and the design anticipates 587 Ah cells. Modules: 100–240 mm high, 150–370 mm wide, 300–1000 mm long. PACKs: 100–250 mm high, 300–800 mm wide, 600–1200 mm long.

    03

    How many operators does the line need?

    About 21: three in cell processing (1 loading, 2 adhesive), six in module stacking and welding (2 strapping, 1 busbar placement, 1 post-weld cleaning, 1 transfer, 1 reserve) and about twelve in PACK assembly.

    04

    What does the plant need to provide?

    A 55 × 9 × 3.5 m footprint (excluding storage and aisles, adaptable to your building), floor load ≥800 kg/m², 380 V ±5 % 50 Hz three-phase five-wire power at 250 kW rated, compressed air at 0.5–0.7 MPa and ≥3000 L/min, and nitrogen at 0.5 MPa and 40 L/min.

    05

    What does "≥99 % yield" cover?

    Line yield of at least 99 % counts defects caused by the equipment only; operator-induced defects are excluded.

    06

    Which operations are automated?

    Automated: depalletizing, cell test and sort, terminal addressing and polarity check, busbar laser welding, module EOL and thermal adhesive dispensing. Semi-automatic: pressing and strapping, cooling-plate leak test, PACK EOL and full-pack leak test. The remaining stations are manual or assisted.

    07

    What are the laser-welding quality figures?

    A 6 kW galvo laser welds at 50–100 mm/s with ≥1.0 mm penetration, ≥1.5 mm width and ≥1000 N pull strength. Cylinder-driven single-point clamping suits both single- and double-row modules.

    08

    Can the line connect to MES?

    Yes. For example, the adhesive dispenser reports pressure and dispensed volume to MES over Profinet and other protocols. Interfaces are confirmed per project.

    09

    Can the layout be adapted to our building?

    Yes. 55 × 9 × 3.5 m is the reference layout; the actual footprint is adapted to your building.

    Put 55 metres of line
    into your plant.

    Share your cell spec, module design and plant constraints. Our engineers will come back with a layout and configuration.